
Uncompromised quality. Certified. At every step.
Our in-house laboratory is equipped with cutting-edge testing equipment to verify that every batch of aluminium foil satisfies the highest global pharmaceutical standards before it ever leaves our facility.
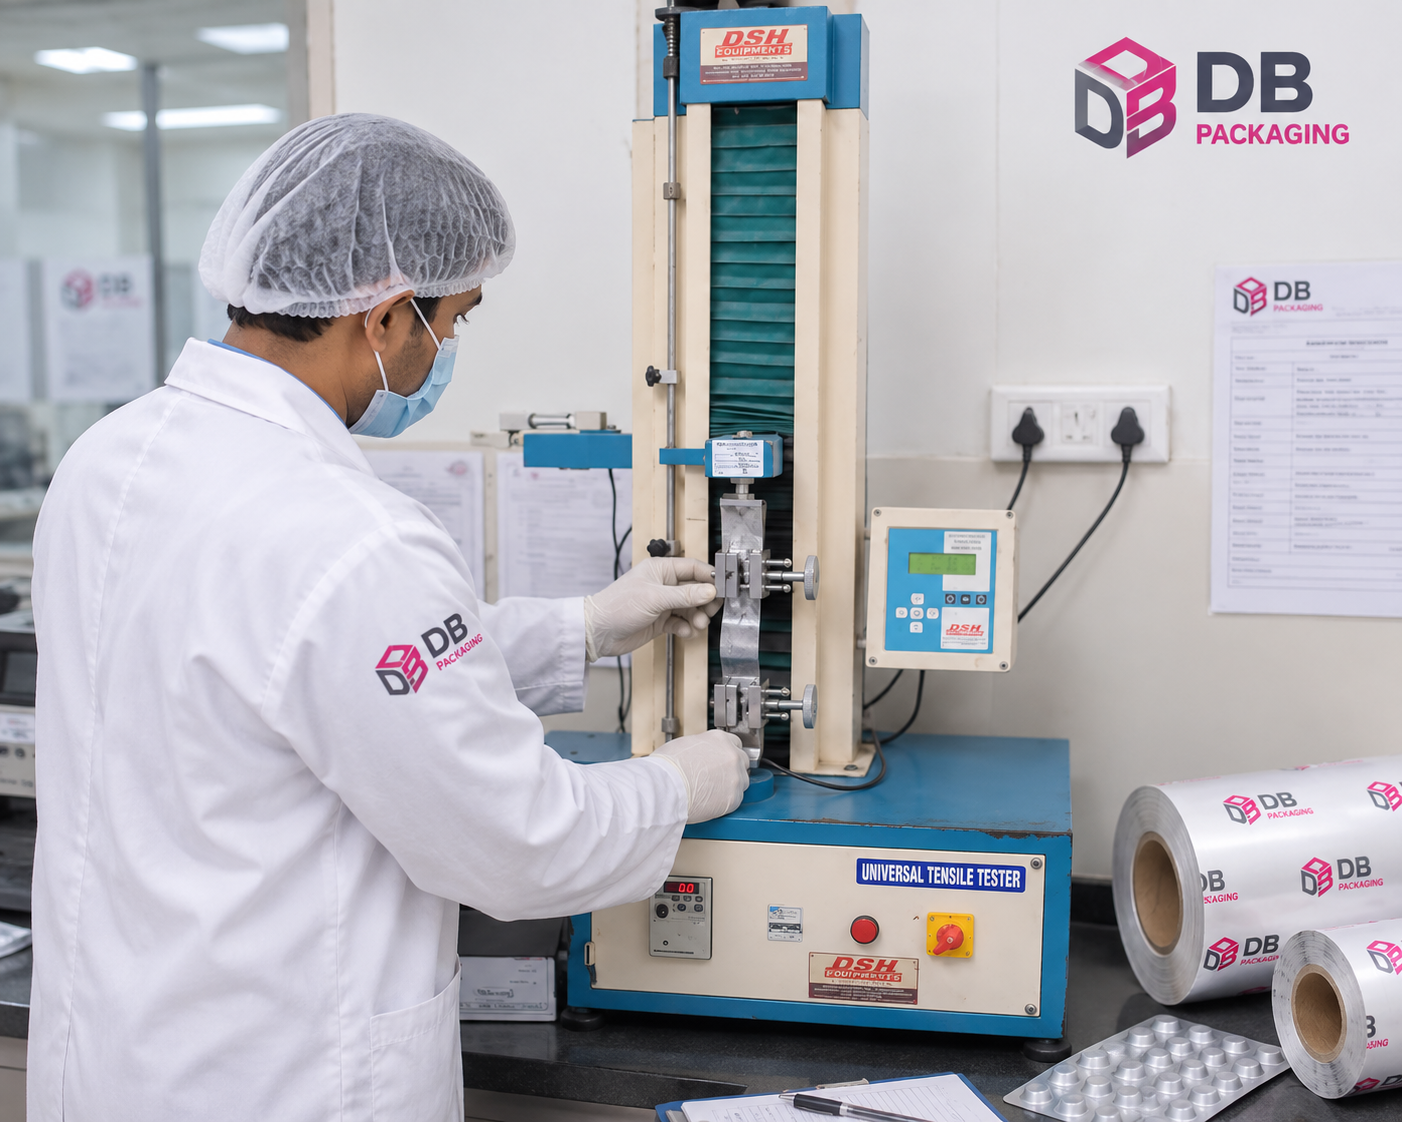
Quality driven at every level of operations.
Our commitment to uncompromised quality drives every aspect of our operations, from raw material intake to final product release, through certified quality management systems and continuously evolving protocols.
We maintain strict compliance with global standards through our certified ISO 9001:2015 Quality Management System, continuously upgrading our protocols to meet evolving regulatory demands.
To ensure maximum product safety and efficiency, we implement rigorous internal controls that completely prevent cross-contamination and product mix-ups. These optimised workflows allow us to deliver exceptional turnaround times from work-order receipt to final delivery.
The foundations behind every batch.
Core pillars underpin our quality promise, from internationally recognised certifications to operational controls that safeguard every product.
ISO 9001:2015
Quality Management System governing our end-to-end process discipline and continual improvement programme.
Zero Cross-Contamination
Rigorous internal controls and segregated workflows completely prevent cross-contamination and product mix-ups at every stage.
Fast Turnaround
Optimised workflows deliver exceptional turnaround times from work-order receipt to final delivery, without compromising on quality.
Stage-wise inspection. Full traceability.
Our advanced in-house QC laboratory is led by experienced quality managers who conduct meticulous, stage-wise process checks, generating comprehensive reports that guarantee full product traceability at every step.
Incoming Material Verification
Every incoming batch of aluminium foil is sampled and evaluated against agreed specifications before it enters the production floor.
Stage-Wise In-Process Checks
Experienced quality managers conduct meticulous checks at each production stage, generating comprehensive inspection records in real time.
Full Product Traceability
Each stage check produces detailed documentation ensuring complete traceability of every batch from receipt through to final release.
Final Release & Certification
Finished reels are cleared only after all defined parameters are satisfied. Certificates and supporting documents are issued as agreed with the customer.
What we measure, and how.
Analytical disciplines supporting a clear inspection trail from incoming checks to finished-reel release.
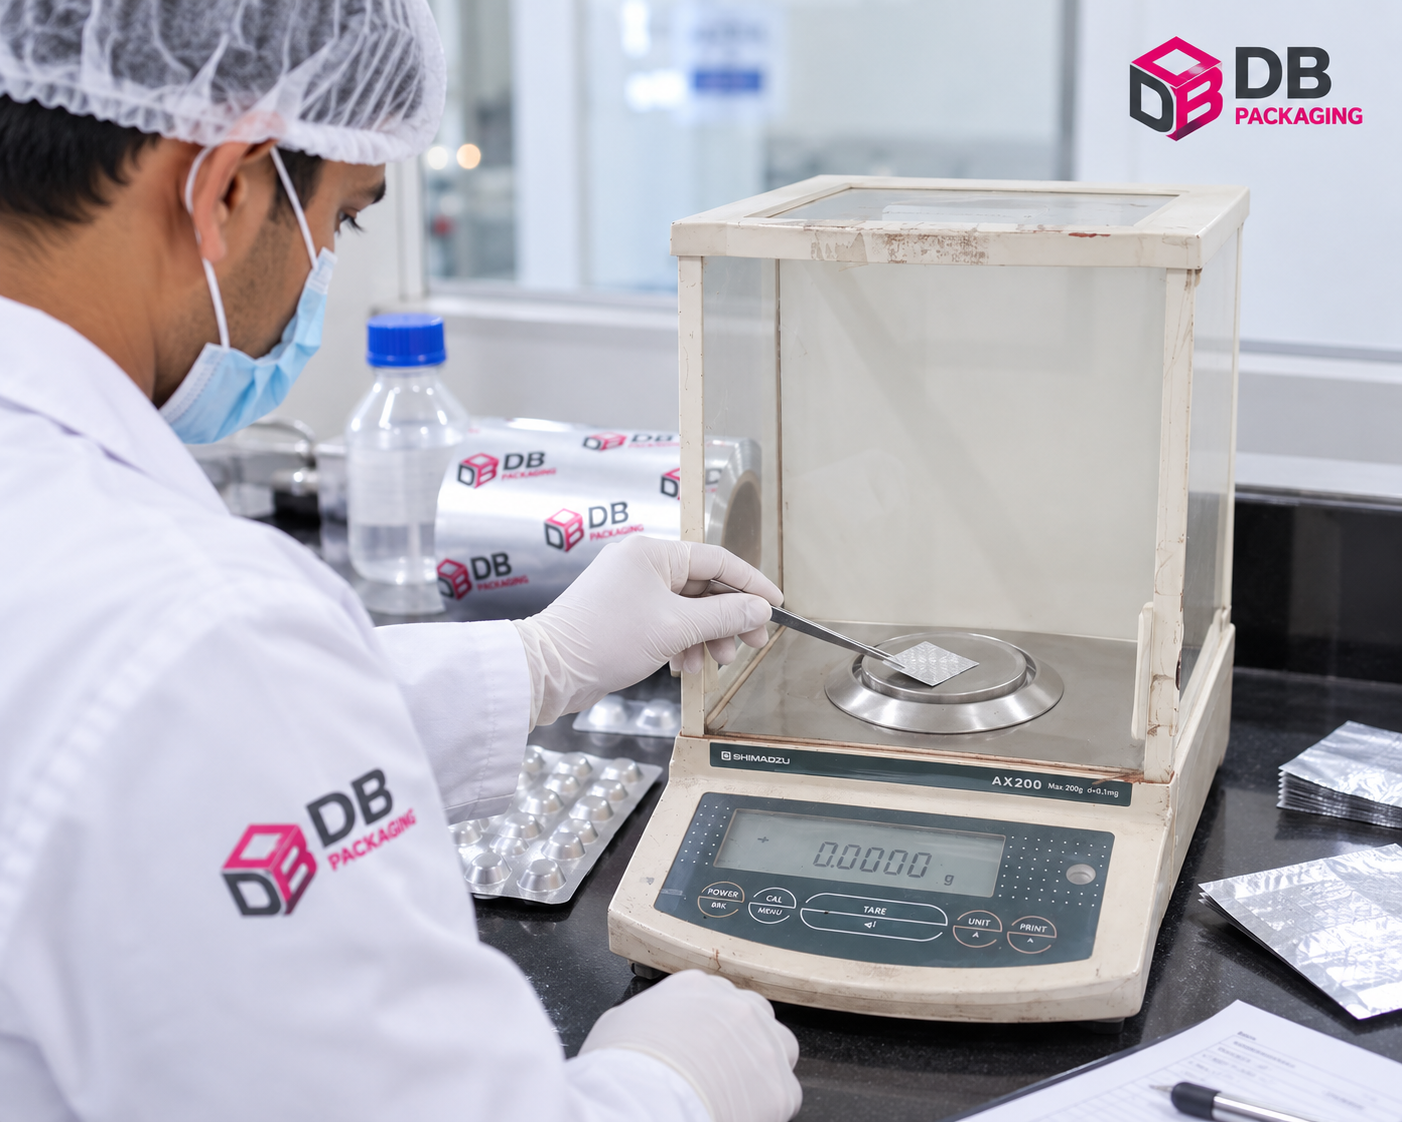
Substrate Inspection
Incoming foil thickness, temper, surface finish and pinhole density per AQL sampling.
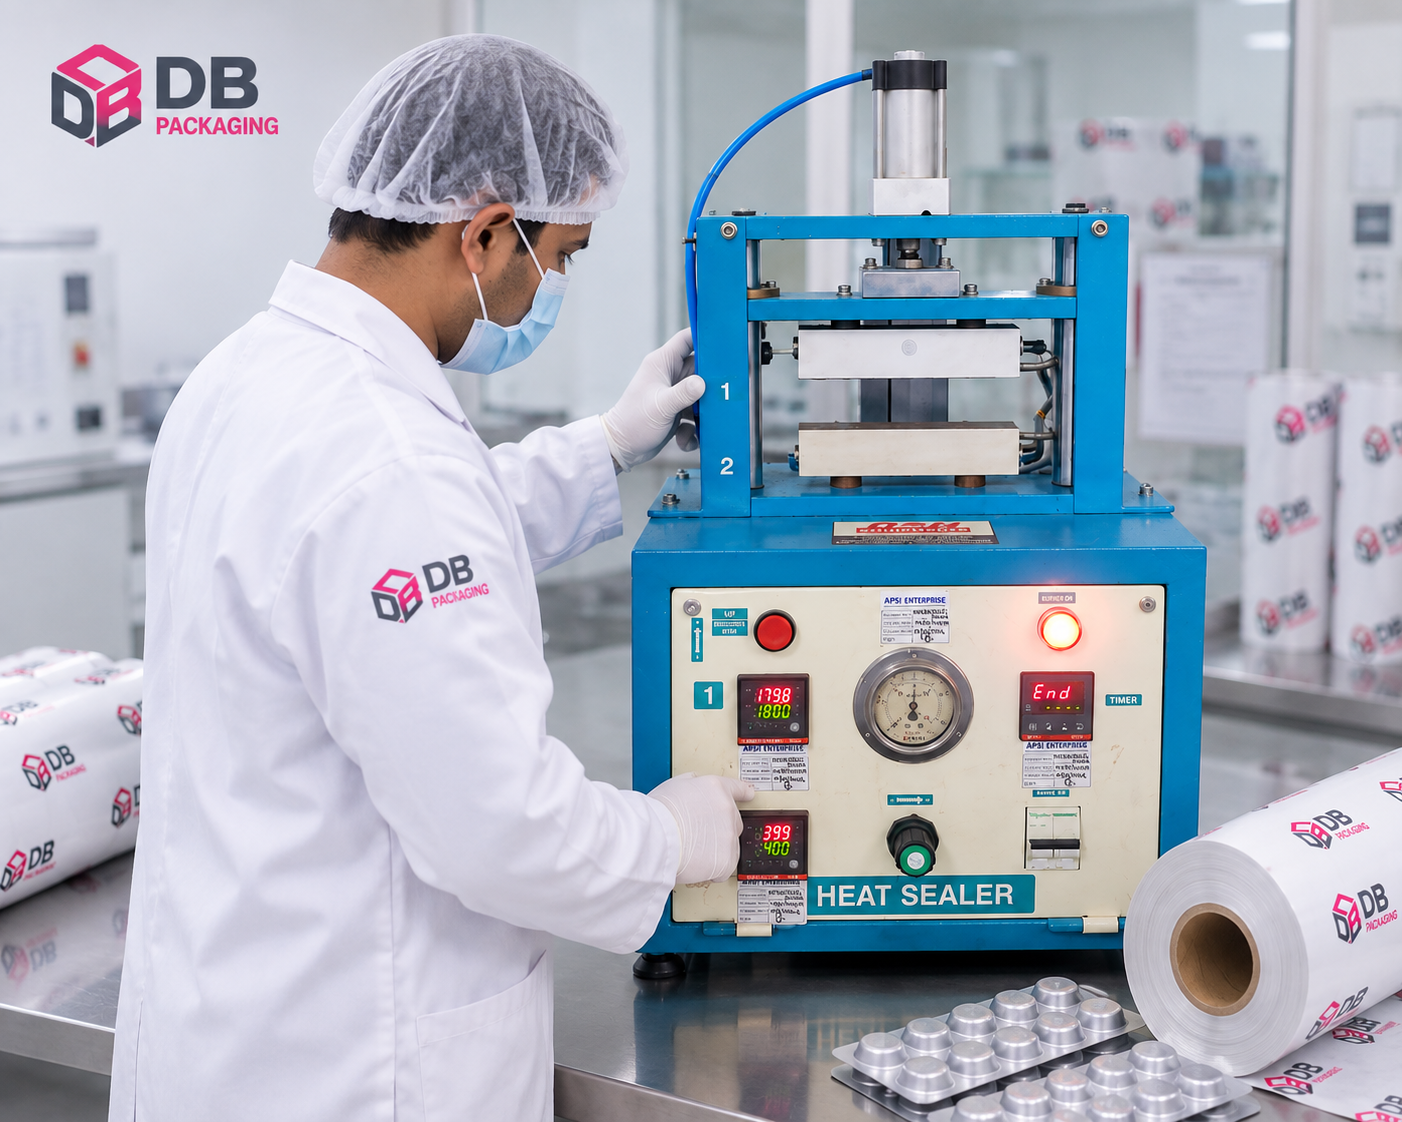
Heat Seal Strength
Pneumatic heat seal testing at multiple seal temperatures and dwell times to ensure seal integrity.
Tensile Strength & Elongation
Tensile testing to evaluate mechanical strength, elongation and foil durability.
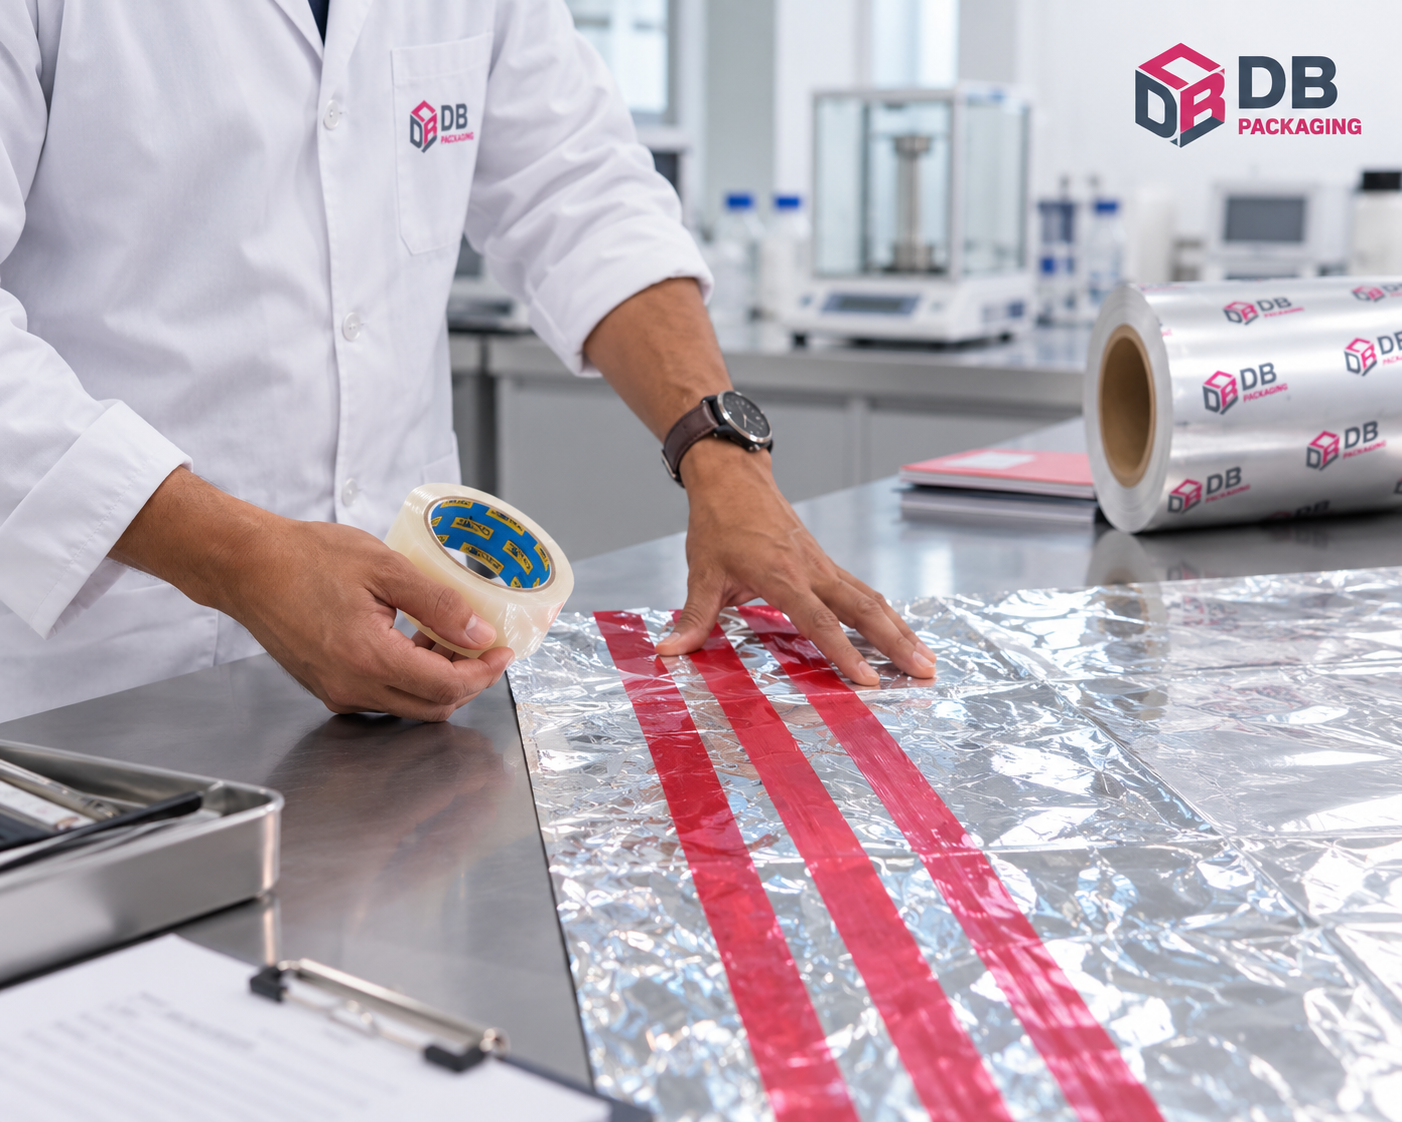
Print Adhesion & Surface Anchorage
Tape test and scratch test on print runs to ensure primer and ink anchorage.
Climate-controlled. Organised. Accountable.
Our QC facility features a dedicated, climate-controlled retention room designed to store and organise controlled retain samples systematically, ensuring long-term batch accountability for every supply we produce.
The systems behind every shipment.
Our Quality Management Systems are certified to the most demanding international standards for pharmaceutical packaging, providing our customers with confidence in every order.
ISO 9001:2015 Certified
Quality Management System accredited by UASL and Quality Control Certification.
Ready to upgrade your primary packaging supplier?
Share your specifications and we'll respond with a technical quotation and sample reels.